Metal Layer and Thin Film Inspection in Semiconductor Manufacturing: Methods and Tools
Averroes
Oct 30, 2026
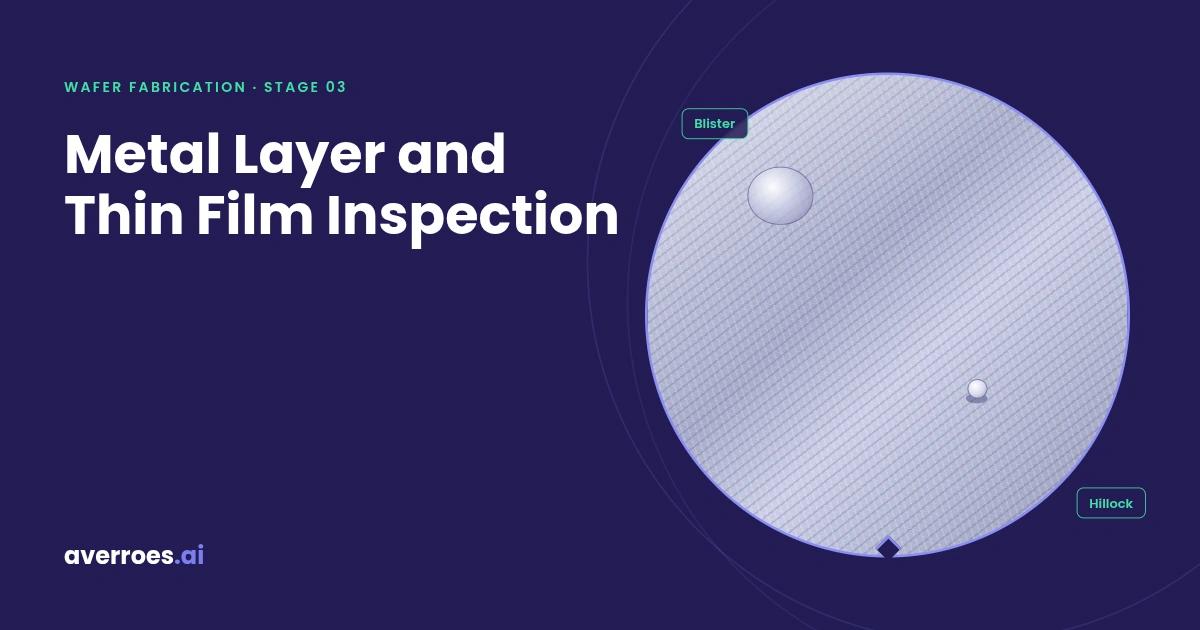
Metal layer and thin film inspection is the inline defect check on deposited films: it finds the particles, splats, pinholes, hillocks, blisters and haze that deposition leaves on metal and dielectric layers. It runs alongside, but distinct from, thin film metrology, which measures a film’s thickness, composition, stress and sheet resistance. Inspection answers whether the film carries defects; metrology answers whether the film is the film the recipe intended.
Film inspection is a per-deposition gate inside Stage 03 of the 12-stage semiconductor manufacturing process. This guide from Averroes.ai, an AI visual inspection platform for manufacturers, separates the two disciplines, maps the deposition defect catalogue to its mechanisms and tools, and explains why reflective metal films are the hardest background in optical inspection.
Key Notes
Film inspection and film metrology answer different questions: inspection finds defects on the film, metrology measures thickness, composition and stress.
Deposition has its own defect catalogue: splats, pinholes, voids, hillocks, blisters and haze, distinct from etch and CMP defects.
A specular metal film is the hardest background in optical inspection: grain and color variation scatter like defects do.
Film stress measured by metrology and the delamination inspection finds are the same problem at two stages.
Film Inspection vs Film Metrology
Thin film inspection finds defects on a deposited film; thin film metrology measures the film itself, its thickness, composition, stress and electrical properties. The two run on the same wafer at the same step, which is why they get blended into one list, and the blend hides the point: they are not substitutes. A film can measure perfectly in thickness, uniformity and stress and still carry killer defects, and a film covered in splats can return a sheet resistance exactly on target.
After deposition: measurement vs inspection
Technique
What It Tells You
Discipline
XRF and XRR
Thickness, composition, density
Metrology
Ellipsometry, reflectometry
Thickness, optical constants
Metrology
Four-point probe
Sheet resistance, resistivity
Metrology
Wafer curvature
Film stress
Metrology
Optical and e-beam inspection
Particles, pinholes, hillocks, delamination
Inspection
The metrology rows are summarized here and covered in depth by the measurement literature; this page covers the inspection row. One correction is worth making explicitly, because merged lists keep repeating it: over-etch and under-etch are pattern-transfer defects, caught at post-etch inspection after the film has been patterned. They are not film defects, and a deposition gate never sees them.
The two disciplines do meet in one place. Wafer-curvature metrology measures the stress a film carries, and that stress is exactly what drives the blistering and delamination that inspection finds. Metrology predicts the risk; inspection catches it when it lands.
The split in one line: metrology asks what the film is, inspection asks what is on it, and a healthy deposition gate needs the answer to both.
Where Film Inspection Sits
Every patterned layer starts as a deposited film: metal deposition in semiconductor manufacturing, by sputtering (PVD), chemical vapor deposition (CVD), atomic layer deposition (ALD) or electrochemical deposition (ECD), lays the material down, and dielectric deposition does the same between the metal levels. Film inspection checks that output before patterning commits it.
The cycle position explains the gate’s economics. The film is deposited, inspected, then patterned at lithography and etch, and for metal levels planarized afterward, where post-CMP inspection takes over. A defect on the deposited film is buried by every layer built above it: a splat under three metal levels cannot be reworked, repaired or often even diagnosed. The deposition gate is the only point where the film is still just a film.
What Defects Does Deposition Leave on a Film?
Deposition defects are flaws created while a film grows: material ejected onto the surface, gaps in coverage, stress-driven protrusions and adhesion failures. Each family points back at a chamber, a target, a recipe or a stress state.
The gallery carries the section’s point: the chamber writes its condition onto the film, and each defect family is a different sentence in that report.
Particles and Splats
Splats are molten droplets ejected onto the growing film by arcing and spitting in a PVD chamber, landing as splashed, irregular mounds. Flaking from chamber walls and shields adds solid particles on top. Both sit proud of the film surface, so both print through the lithography and deposition that follow, turning one deposition event into defects on several layers.
Pinholes and Voids
A pinhole defect in a thin film is a gap in coverage: a spot where the film failed to nucleate, was shadowed by a particle, or was opened by contamination. In most films a pinhole is a visual defect; in a barrier or seed layer it is a reliability failure, because the material above it now touches the material below it. Voids are the buried version, trapped inside the film rather than open at its surface.
Hillocks and Whiskers
A hillock defect is a stress-driven protrusion pushed up out of the film, classically from aluminum under compressive stress during thermal cycling. Whiskers are the same relief mechanism grown long and thin. A hillock tall enough to reach the layer above becomes a short, and an outbreak of them across a wafer is a stress signature, not a particle problem: the fix is in the film and its thermal history, not the chamber clean.
Blistering and Delamination
Film delamination is adhesion failure: the film’s stress exceeds its grip on the surface below, and it lifts. Blisters are the local, domed version; peeling is the regional one. This is the inspection-side twin of the stress that wafer-curvature metrology measures, and a rising blister count on one film stack is usually a stress or surface-preparation drift announcing itself.
Haze and Roughness
Haze on a deposited film is scattering from its microstructure: grain size, texture and roughness rather than any single defect. It reads two ways at once. As a signal, wrong haze means wrong microstructure, often a drifting process. As noise, haze raises the background that every later inspection of this wafer has to see through, which makes it a defect source and a nuisance source in the same measurement.
How Deposited Films Are Inspected
Film inspection runs on two surfaces: blanket monitor wafers that qualify the deposition tool, and patterned product wafers where the film has become the device.
The two surfaces divide the work: the blanket wafer isolates what the chamber adds, and the product wafer shows what the film does once it carries the device.
Blanket Film Inspection
Blanket inspection scans unpatterned monitor wafers after deposition runs, using dark field inspection and its haze channel. With no pattern on the surface, everything detected came from the deposition itself, which makes blanket monitors the cleanest read on chamber health: arcing signatures, flaking particles and haze drift all show here first, and tool qualification and requalification run on exactly this measurement.
Patterned Metal Layer Inspection
Patterned inspection runs on product, where the film sits over topography and carries a pattern. Bright field inspection and darkfield compare die against die to find the splats, pinholes and blisters that landed on real devices, plus anything the pattern transfer has already revealed. The surface is no longer uniform, which changes the problem entirely.
The Reflective-Surface Problem
A specular metal film is the hard case in optical inspection. A freshly deposited metal surface mirrors light, its grain structure scatters it, and its color and apparent brightness shift with small thickness variations, so the background itself behaves the way defects do. Metal layers run the highest nuisance rates in the fab for exactly this reason, and the standard accommodation, turning sensitivity down until the noise is bearable, is capture given away on the layers where a short or an open costs the most.
The comparison makes the argument visible: the defects are identical on both surfaces, and only one background keeps them obvious.
Where AI Detection Fits on Metal Layers
AI defect detection learns the film’s own background, grain, color and pattern, so detection sensitivity no longer has to be traded away against metal-surface noise. On reflective, grainy films the limiting factor is rarely the optics; it is the background model deciding what counts as signal. A learned model carries the film’s normal appearance, which lets the tools run at full sensitivity while real splats, pinholes, hillocks and blisters separate from grain sparkle and color variation. Classification behind it keeps the review queue honest, so nuisance stops consuming the attention the real detections need.
Averroes.ai runs as an overlay on the blanket and patterned inspection tools already installed at the deposition gate. AI defect detection runs on the reflective film imagery those tools produce, with AI defect classification sorting detections behind it, trained from 20 to 40 labeled images per defect class, with no code, deployed on premise so wafer image data stays inside the fab. It augments the installed inspection tools; it does not replace them.
Grain Noise Drowning Out Real Defects?
See AI defect detection on your own thin film inspection images
Frequently Asked Questions
What is thin film inspection in semiconductor manufacturing?
Thin film inspection is the inline defect check on deposited metal and dielectric films, run on blanket monitor wafers and patterned product. It finds the particles, splats, pinholes, hillocks, blisters and haze that deposition leaves behind, before lithography and etch pattern the film and later layers bury whatever it carried.
What is the difference between thin film inspection and thin film metrology?
Thin film metrology measures the film: thickness, composition, stress and sheet resistance, by techniques such as ellipsometry, XRF and the four-point probe. Thin film inspection finds defects on the film. The two are not substitutes, because a film can measure exactly in spec and still carry killer defects on its surface.
What defects occur during thin film deposition?
Deposition defects include particles and splats from chamber arcing and flaking, pinholes and voids where coverage failed, hillocks and whiskers pushed up by film stress, blistering and delamination where adhesion lost to stress, and haze from the film’s own microstructure. Each family points back at a chamber condition, recipe or stress state.
What is a hillock defect?
A hillock defect is a protrusion pushed up out of a metal film by compressive stress, classically on aluminum during thermal cycling. A hillock tall enough to reach the layer above becomes an electrical short. An outbreak of hillocks is a stress signature, so the fix lies in the film stack and its thermal history rather than in chamber cleaning.
What causes film delamination?
Film delamination happens when the stress a film carries exceeds its adhesion to the surface below, so the film lifts as blisters or peels away in regions. Poor surface preparation, contamination at the interface and high intrinsic or thermal stress all drive it. The stress that wafer-curvature metrology measures is the same stress behind the blisters inspection finds.
What is a pinhole defect in a thin film?
A pinhole defect is a small gap in film coverage, left by shadowing from a particle, failed nucleation or contamination. In most films it is a surface defect; in a barrier or seed layer it is a reliability failure, because the materials the film was meant to separate now touch through the gap.




Metal layer and thin film inspection is the inline defect check on deposited films: it finds the particles, splats, pinholes, hillocks, blisters and haze that deposition leaves on metal and dielectric layers. It runs alongside, but distinct from, thin film metrology, which measures a film’s thickness, composition, stress and sheet resistance. Inspection answers whether the film carries defects; metrology answers whether the film is the film the recipe intended.
Film inspection is a per-deposition gate inside Stage 03 of the 12-stage semiconductor manufacturing process. This guide from Averroes.ai, an AI visual inspection platform for manufacturers, separates the two disciplines, maps the deposition defect catalogue to its mechanisms and tools, and explains why reflective metal films are the hardest background in optical inspection.
Key Notes
Film Inspection vs Film Metrology
Thin film inspection finds defects on a deposited film; thin film metrology measures the film itself, its thickness, composition, stress and electrical properties. The two run on the same wafer at the same step, which is why they get blended into one list, and the blend hides the point: they are not substitutes. A film can measure perfectly in thickness, uniformity and stress and still carry killer defects, and a film covered in splats can return a sheet resistance exactly on target.
After deposition: measurement vs inspection
The metrology rows are summarized here and covered in depth by the measurement literature; this page covers the inspection row. One correction is worth making explicitly, because merged lists keep repeating it: over-etch and under-etch are pattern-transfer defects, caught at post-etch inspection after the film has been patterned. They are not film defects, and a deposition gate never sees them.
The two disciplines do meet in one place. Wafer-curvature metrology measures the stress a film carries, and that stress is exactly what drives the blistering and delamination that inspection finds. Metrology predicts the risk; inspection catches it when it lands.
The split in one line: metrology asks what the film is, inspection asks what is on it, and a healthy deposition gate needs the answer to both.
Where Film Inspection Sits
Every patterned layer starts as a deposited film: metal deposition in semiconductor manufacturing, by sputtering (PVD), chemical vapor deposition (CVD), atomic layer deposition (ALD) or electrochemical deposition (ECD), lays the material down, and dielectric deposition does the same between the metal levels. Film inspection checks that output before patterning commits it.
The cycle position explains the gate’s economics. The film is deposited, inspected, then patterned at lithography and etch, and for metal levels planarized afterward, where post-CMP inspection takes over. A defect on the deposited film is buried by every layer built above it: a splat under three metal levels cannot be reworked, repaired or often even diagnosed. The deposition gate is the only point where the film is still just a film.
What Defects Does Deposition Leave on a Film?
Deposition defects are flaws created while a film grows: material ejected onto the surface, gaps in coverage, stress-driven protrusions and adhesion failures. Each family points back at a chamber, a target, a recipe or a stress state.
The gallery carries the section’s point: the chamber writes its condition onto the film, and each defect family is a different sentence in that report.
Particles and Splats
Splats are molten droplets ejected onto the growing film by arcing and spitting in a PVD chamber, landing as splashed, irregular mounds. Flaking from chamber walls and shields adds solid particles on top. Both sit proud of the film surface, so both print through the lithography and deposition that follow, turning one deposition event into defects on several layers.
Pinholes and Voids
A pinhole defect in a thin film is a gap in coverage: a spot where the film failed to nucleate, was shadowed by a particle, or was opened by contamination. In most films a pinhole is a visual defect; in a barrier or seed layer it is a reliability failure, because the material above it now touches the material below it. Voids are the buried version, trapped inside the film rather than open at its surface.
Hillocks and Whiskers
A hillock defect is a stress-driven protrusion pushed up out of the film, classically from aluminum under compressive stress during thermal cycling. Whiskers are the same relief mechanism grown long and thin. A hillock tall enough to reach the layer above becomes a short, and an outbreak of them across a wafer is a stress signature, not a particle problem: the fix is in the film and its thermal history, not the chamber clean.
Blistering and Delamination
Film delamination is adhesion failure: the film’s stress exceeds its grip on the surface below, and it lifts. Blisters are the local, domed version; peeling is the regional one. This is the inspection-side twin of the stress that wafer-curvature metrology measures, and a rising blister count on one film stack is usually a stress or surface-preparation drift announcing itself.
Haze and Roughness
Haze on a deposited film is scattering from its microstructure: grain size, texture and roughness rather than any single defect. It reads two ways at once. As a signal, wrong haze means wrong microstructure, often a drifting process. As noise, haze raises the background that every later inspection of this wafer has to see through, which makes it a defect source and a nuisance source in the same measurement.
How Deposited Films Are Inspected
Film inspection runs on two surfaces: blanket monitor wafers that qualify the deposition tool, and patterned product wafers where the film has become the device.
The two surfaces divide the work: the blanket wafer isolates what the chamber adds, and the product wafer shows what the film does once it carries the device.
Blanket Film Inspection
Blanket inspection scans unpatterned monitor wafers after deposition runs, using dark field inspection and its haze channel. With no pattern on the surface, everything detected came from the deposition itself, which makes blanket monitors the cleanest read on chamber health: arcing signatures, flaking particles and haze drift all show here first, and tool qualification and requalification run on exactly this measurement.
Patterned Metal Layer Inspection
Patterned inspection runs on product, where the film sits over topography and carries a pattern. Bright field inspection and darkfield compare die against die to find the splats, pinholes and blisters that landed on real devices, plus anything the pattern transfer has already revealed. The surface is no longer uniform, which changes the problem entirely.
The Reflective-Surface Problem
A specular metal film is the hard case in optical inspection. A freshly deposited metal surface mirrors light, its grain structure scatters it, and its color and apparent brightness shift with small thickness variations, so the background itself behaves the way defects do. Metal layers run the highest nuisance rates in the fab for exactly this reason, and the standard accommodation, turning sensitivity down until the noise is bearable, is capture given away on the layers where a short or an open costs the most.
The comparison makes the argument visible: the defects are identical on both surfaces, and only one background keeps them obvious.
Where AI Detection Fits on Metal Layers
AI defect detection learns the film’s own background, grain, color and pattern, so detection sensitivity no longer has to be traded away against metal-surface noise. On reflective, grainy films the limiting factor is rarely the optics; it is the background model deciding what counts as signal. A learned model carries the film’s normal appearance, which lets the tools run at full sensitivity while real splats, pinholes, hillocks and blisters separate from grain sparkle and color variation. Classification behind it keeps the review queue honest, so nuisance stops consuming the attention the real detections need.
Averroes.ai runs as an overlay on the blanket and patterned inspection tools already installed at the deposition gate. AI defect detection runs on the reflective film imagery those tools produce, with AI defect classification sorting detections behind it, trained from 20 to 40 labeled images per defect class, with no code, deployed on premise so wafer image data stays inside the fab. It augments the installed inspection tools; it does not replace them.
Grain Noise Drowning Out Real Defects?
See AI defect detection on your own thin film inspection images
Frequently Asked Questions
What is thin film inspection in semiconductor manufacturing?
Thin film inspection is the inline defect check on deposited metal and dielectric films, run on blanket monitor wafers and patterned product. It finds the particles, splats, pinholes, hillocks, blisters and haze that deposition leaves behind, before lithography and etch pattern the film and later layers bury whatever it carried.
What is the difference between thin film inspection and thin film metrology?
Thin film metrology measures the film: thickness, composition, stress and sheet resistance, by techniques such as ellipsometry, XRF and the four-point probe. Thin film inspection finds defects on the film. The two are not substitutes, because a film can measure exactly in spec and still carry killer defects on its surface.
What defects occur during thin film deposition?
Deposition defects include particles and splats from chamber arcing and flaking, pinholes and voids where coverage failed, hillocks and whiskers pushed up by film stress, blistering and delamination where adhesion lost to stress, and haze from the film’s own microstructure. Each family points back at a chamber condition, recipe or stress state.
What is a hillock defect?
A hillock defect is a protrusion pushed up out of a metal film by compressive stress, classically on aluminum during thermal cycling. A hillock tall enough to reach the layer above becomes an electrical short. An outbreak of hillocks is a stress signature, so the fix lies in the film stack and its thermal history rather than in chamber cleaning.
What causes film delamination?
Film delamination happens when the stress a film carries exceeds its adhesion to the surface below, so the film lifts as blisters or peels away in regions. Poor surface preparation, contamination at the interface and high intrinsic or thermal stress all drive it. The stress that wafer-curvature metrology measures is the same stress behind the blisters inspection finds.
What is a pinhole defect in a thin film?
A pinhole defect is a small gap in film coverage, left by shadowing from a particle, failed nucleation or contamination. In most films it is a surface defect; in a barrier or seed layer it is a reliability failure, because the materials the film was meant to separate now touch through the gap.